
Industries
Automotive Components & Tires
Connect machine-fleet process data, product identities, and group-level collaboration into a verifiable traceability chain
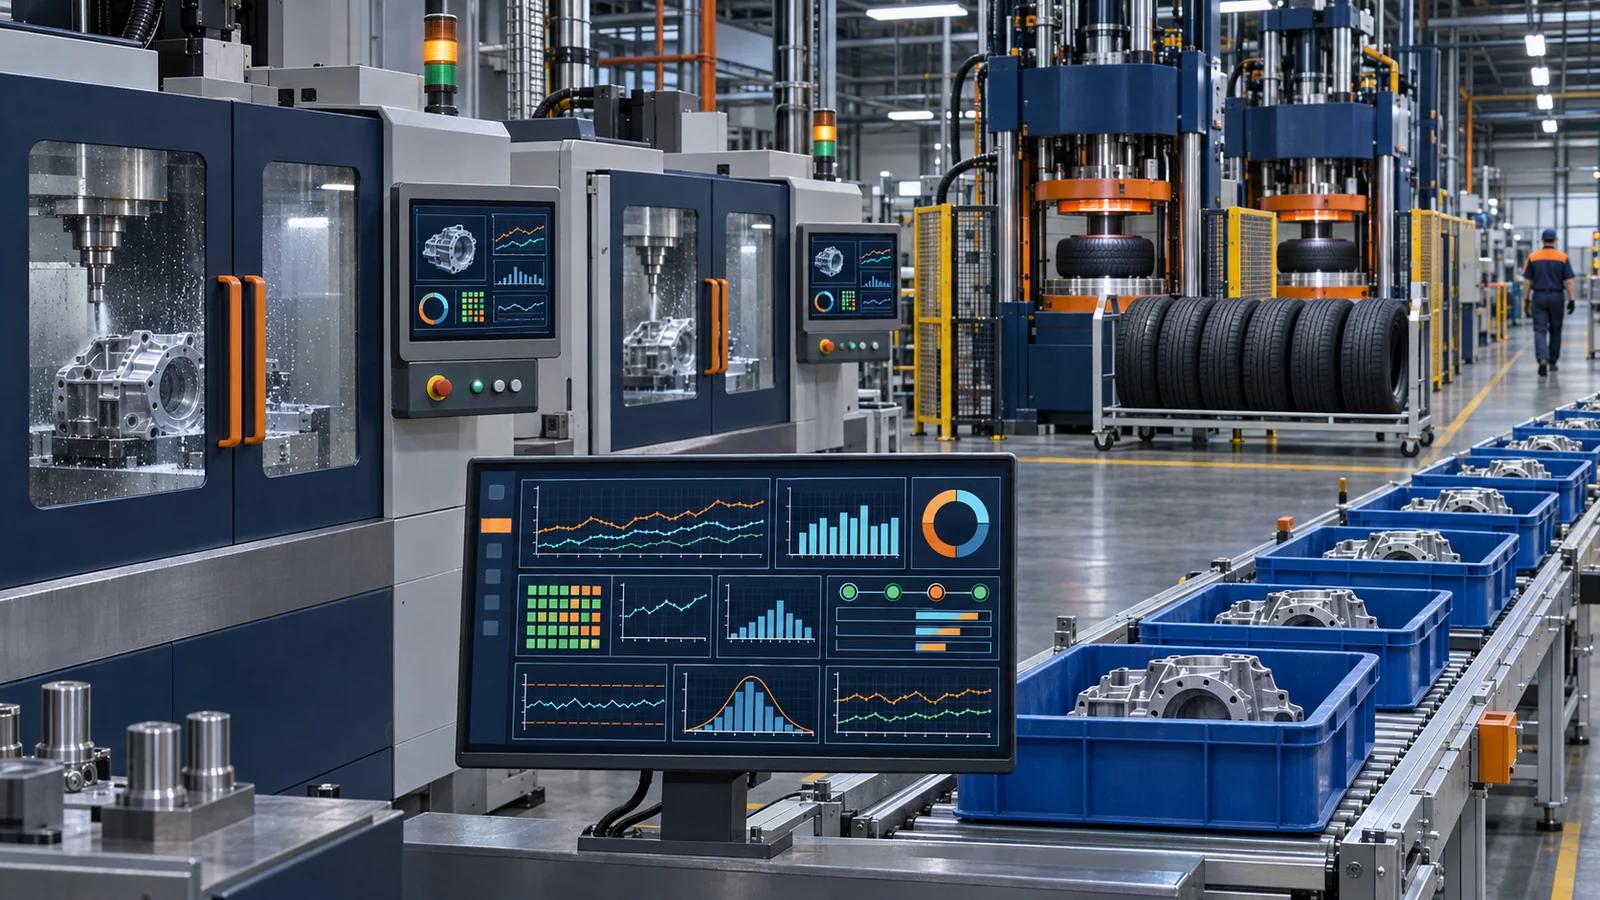
Automotive component and tire production is characterized by large equipment fleets, continuous processes, detailed quality-evidence requirements, and multi-site coordination. Shanghai Orpaon links equipment connectivity, process curves, execution records, and product barcodes, with particular attention to data integrity during network outages, master data across systems, and template boundaries between sites.
Typical challenges
- Curing presses, tire building machines, test benches, and assembly equipment use different protocols, making it difficult to standardize tag lists, sampling cycles, and clocks across the fleet.
- Process curves and execution records can develop gaps during network outages; if only live values are accepted after recovery, the process cannot be reconstructed.
- Without stable links among barcodes, molds, machines, process curves, and inspection results, both forward tracing and backward investigation rely on manual work.
- When enterprise and shop-floor systems lack clear data ownership, work orders, materials, process versions, and result write-backs are prone to duplicate maintenance.
- Sites differ in equipment generations, networks, and operating practices; copying programs directly can cause interface and definition drift.
Solution approach
Unified Equipment Fleet Connectivity
Create protocol adapters, tag-list templates, sampling strategies, and status models by equipment family. Use sampling cycles suited to critical processes, and identify silent tags and abnormal values through connection monitoring and data-quality checks.
Offline Buffering and Post-Recovery Backfill
Define the data scope, sequence identifiers, and retention conditions that can be buffered at the equipment or edge layer. After communications recover, backfill in chronological order and check for duplicates, gaps, and causal consistency. Actual capabilities must be validated against equipment buffering and site links.
Curing MES and Process Execution
Organize curing execution around work orders, machines, barcodes, recipes or process versions, process curves, and completion records. Exception handling and release responsibilities remain configured and accepted according to the plant's established procedures.
Forward and Backward Quality Traceability
Use a common product key to link raw-material or upstream identities, machines, tooling, personnel, process curves, and inspection results, supporting both product-to-process review and identification of affected products from abnormal conditions.
Enterprise Interfaces and Multi-Site Templates
Define object ownership, interface triggers, and failure compensation between MES and existing systems such as ERP. Separate the common data model from site-specific configuration, validate a reference implementation, and then replicate it site by site.
Implementation
- 1.
Inventory the Fleet and Master Data
Inventory equipment families, controllers, process curves, product identifiers, molds, and enterprise-system objects, and specify which system maintains each field.
- 2.
Validate Acquisition and Outage Scenarios
Select representative machines to test normal acquisition, communication interruptions, post-recovery backfill, duplicate removal, and clock synchronization, producing reproducible acceptance test cases.
- 3.
Connect Execution and Traceability in One Area
Within a defined area, connect work orders to machines, processes to barcodes, and inspections to products, then validate forward and backward queries and exception handling.
- 4.
Integrate Enterprise-System Interfaces
Validate master-data distribution, execution write-backs, interface retry after failure, and reconciliation, avoiding manual duplicate entry that obscures unclear interface responsibilities.
- 5.
Replicate After Reference Acceptance
Standardize equipment-family templates, interface specifications, test cases, and training materials. Revalidate networks, equipment versions, and local business differences when replicating to other sites.
Frequently asked questions
Does post-outage backfill mean all historical data can always be recovered?
No. Backfill depends on whether the equipment or edge layer retained data during the outage, buffer capacity, the reliability of timestamps and sequence numbers, and the read mechanism available after recovery. The project must validate the recoverable scope using real disconnection scenarios and define how unrecoverable gaps are flagged and handled.
Must every process tag be acquired for traceability?
The acquisition scope should be determined by quality risks, process-analysis objectives, storage constraints, and query scenarios. Define the process evidence that must be reconstructed first, then identify critical tags, curves, and events. Unbounded acquisition can create large volumes of unusable data.
Can multi-site replication simply install the same program everywhere?
Data models, interface specifications, common functions, and acceptance methods can be reused, but differences in equipment versions, tag lists, network zoning, master data, and operating rules must not be overlooked. Each site still requires adaptation checks and on-site acceptance.
Do ERP work orders and materials still need to be maintained after MES goes live?
That depends on system-of-record design. Typically, the enterprise and shop-floor systems are assigned responsibility for specific objects and states, synchronized through interfaces with reconciliation. MES should not be expected to replicate or replace all ERP functions unconditionally.
Related products
Machine Data Acquisition and Production-Line Connectivity
Capture data from mixed-vendor equipment accurately and reliably before reusing it for monitoring, traceability, and analysis
Production-Line MES and Quality Traceability
Ground work-order execution in evidence, record process exceptions, and make product genealogy traceable

Validate One Complete Curing Traceability Chain First
Start with three critical scenarios: the equipment tag list, recovery after a network outage, and barcode association. Confirm the reference area and the technical boundaries for subsequent replication.